China Best Textile Dyeing Process for Global Buyers?

China Best Textile Dyeing Process for Global Buyers? The answer depends on chemistry, fiber type, equipment, and verified factory controls. Dyeing is not simply adding color. It involves pretreatment, bath preparation, temperature control, fixation, washing, drying, and wastewater management.

Professor M. L. Gulrajani, a leading textile coloration scholar, describes dyeing as “the coloration of a textile material with a dye.” This practical definition remains important for buyers. A stable shade requires controlled pH, water hardness, salt concentration, and processing time. A small error can create streaks, poor fastness, or costly rework. The dye bath tells the truth.

Industry data shows why the process deserves close attention. Textile Exchange’s Materials Market Report 2024 reported global fiber production of approximately 132 million tonnes in 2023. It may reach about 160 million tonnes by 2030. The United Nations Environment Programme also identifies textile production as a major pressure on water, chemicals, and energy resources. However, some industry statistics use different boundaries. Buyers should question dramatic percentages before accepting them.

A reliable Chinese supplier should provide lab-dip records, colorfastness results, chemical inventories, and wastewater test reports. Certifications such as OEKO-TEX Standard 100, bluesign, and ZDHC alignment can support verification. They do not replace factory audits.

The best textile industry dyeing process is therefore not one universal recipe. Reactive dyeing suits many cotton fabrics, while disperse dyeing serves polyester. Low-liquor machines can reduce water use, but poor process control may reduce quality. Global buyers should compare measured performance, not attractive claims. Perfect sustainability is unrealistic; documented improvement is more credible.
China Best Textile Dyeing Process for Global Buyers?

Textile Dyeing in China: Processes, Materials, and Production Standards

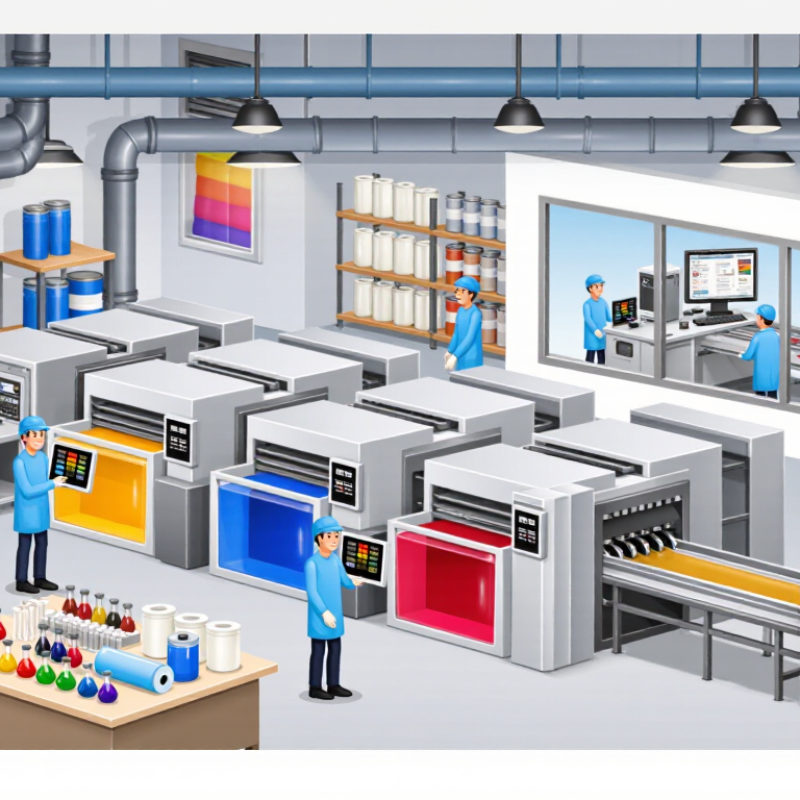
China’s textile dyeing process combines fiber preparation, color formulation, dyeing, washing, drying, and finishing. Polyester commonly uses disperse dyes at high temperatures, while cotton often uses reactive dyes with salt and controlled alkali. According to Textile Exchange’s Materials Market Report 2024, global fiber production reached about 124 million tonnes in 2023, and polyester represented roughly 57%. This scale makes batch control essential for global buyers. A practical factory check should compare laboratory dips with bulk fabric under identical light sources. Small shade differences can appear after washing.

Production standards must cover more than color matching. Quality teams typically monitor pH, temperature curves, liquor ratio, shrinkage, colorfastness, and wastewater records. ISO 105 test methods help evaluate washing, rubbing, and perspiration fastness, while ISO 9001 supports documented quality management. UNEP reports that textiles generate around 2–8% of global greenhouse-gas emissions and consume approximately 215 trillion liters of water annually. Therefore, low-liquor machines, water reuse, and safer chemical inventories deserve attention during supplier audits. Certification alone is not enough. A document may be current, but the production floor can still drift. Buyers should request test reports, random bulk samples, corrective-action records, and traceable batch numbers before approving shipment. Dyeing remains a technical process with human judgment, and that judgment sometimes needs stronger verification.
How Chinese Textile Dyeing Works from Preparation to Finishing

China’s Best Textile Dyeing Process for Global Buyers

How Chinese Textile Dyeing Works from Preparation to Finishing

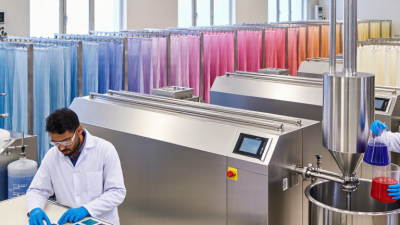
China’s textile dyeing process starts long before fabric enters a machine. Technicians inspect fiber type, yarn density, absorbency, and grey-fabric defects. Preparation removes oils, sizing agents, and natural impurities through desizing, scouring, and controlled bleaching. Cotton often uses reactive dyes, while polyester commonly requires disperse dyes at high temperature. This choice affects shade, energy use, and colorfastness. Textile Exchange’s 2024 Materials Market Report states polyester represented about 57% of global fiber production in 2023. That figure makes polyester dyeing knowledge essential for global buyers.

A Chinese dyehouse normally runs a lab dip before bulk production. Operators adjust liquor ratio, temperature curves, salt, alkali, and dye concentration. The approved swatch becomes the production reference, but it is not a guarantee. Water quality, machine loading, and fabric tension can still shift the shade. Buyers should request Delta E limits, wash and rubbing fastness results, shrinkage data, and lot-to-lot records. ISO 105 methods and AATCC procedures provide useful testing frameworks. In practice, rushed lab-dip approval creates more problems than weak dye chemistry.

After dyeing, washing removes unfixed color and chemicals. Finishing may add softness, water repellency, anti-pilling performance, or dimensional stability. Drying and stentering must control width, weight, and hand feel. The World Bank has cited textile dyeing as responsible for about 20% of global wastewater. Therefore, credible suppliers should show wastewater treatment data, chemical management records, and corrective actions. No batch is perfect. Good factories measure variation, explain it, and improve the next run.

This chart shows representative temperature ranges used in a cotton reactive-dyeing workflow, from preparation to finishing. Actual settings vary according to fiber type, dye chemistry, fabric construction, and equipment.

Major Dyeing Methods Used by Chinese Textile Manufacturers

Chinese textile manufacturers commonly select dyeing methods according to fiber type, order volume, color depth, and delivery requirements. Fiber dyeing colors polyester, nylon, or other fibers before spinning. It creates blended effects and can improve shade consistency. However, it may reduce flexibility when buyers later change colors.

Yarn dyeing colors the yarn before weaving or knitting. It suits stripes, checks, jacquards, and engineered patterns. Operators must control yarn tension carefully. Uneven tension can create visible bands after fabric formation. Piece dyeing is more widely used for solid fabrics because it supports flexible production. Reactive dyes are common for cotton and other cellulosic fibers. They offer strong color performance when washing, salt levels, temperature, and fixation time are controlled. Disperse dyes are used mainly for polyester. They require high-temperature equipment and careful reduction clearing.

Pigment dyeing coats color onto the fabric surface instead of forming the same chemical bond as reactive dyeing. It can create a dry, vintage appearance and reduce water use in some processes. The trade-off is possible crocking or a stiffer hand feel. I have found that laboratory samples can look excellent, while bulk fabric reveals small shade differences. This is why reliable manufacturers compare lab dips, bulk swatches, and wash-test results. Buyers should request data on colorfastness, shrinkage, pH, and restricted substances before approving production. Dyeing is not only a color decision. It is a process-control decision.

China Best Textile Dyeing Process for Global Buyers? - Major Dyeing Methods Used by Chinese Textile Manufacturers
Dyeing Method Typical Fiber or Fabric Common Process Temperature Key Process Features Main Advantages Important Buyer Considerations Typical Color Fastness Profile
Reactive Dyeing Cotton Viscose Lyocell Linen Usually 40–80°C, depending on the reactive dye class and fabric construction. Uses salt to promote dye exhaustion and an alkaline agent to fix the dye chemically to the cellulose fiber. Thorough washing and soaping are required after fixation. Wide color range, bright shades, good wash fastness, and strong suitability for mass-market cellulosic fabrics. Salt and alkali loading can increase wastewater treatment requirements. Ask for fixation efficiency, washing procedure, restricted-substance test results, and color reproducibility data. Generally good wash fastness; light fastness varies by shade and dye selection. Dark and brilliant shades require careful after-washing.
Disperse Dyeing Polyester Polyester Blends Microfiber High-temperature dyeing is commonly performed at approximately 120–135°C under pressure. Carrier dyeing may use lower temperatures for selected constructions. Uses water-insoluble disperse dyes that diffuse into hydrophobic polyester fibers. Reduction clearing is often used to remove unfixed surface dye. Excellent suitability for polyester, strong shade build-up, and good production consistency when temperature and liquor circulation are controlled. High-temperature equipment is required for most polyester articles. Control oligomers, dye migration, sublimation behavior, and reduction-clearing wastewater. Usually good wash fastness. Light fastness and sublimation fastness depend strongly on dye chemistry, shade, and finishing temperature.
Acid Dyeing Nylon Wool Silk Polyamide Commonly 80–100°C, with pH adjusted according to the fiber and acid-dye type. Operates in an acidic bath. Dye uptake is controlled through pH, temperature ramp, leveling agents, and bath circulation. Good leveling potential, vivid colors, and compatibility with protein fibers and polyamide materials. Excessive heat or unsuitable pH can damage wool, silk, or elastic components. Confirm shade tolerance, pH control, and compatibility with blended fabrics. Wash fastness is generally moderate to good; light fastness varies by dye class and color depth.
Vat Dyeing Cotton Cellulosic Fabrics Denim Many vat-dyeing stages operate around 50–70°C, although the exact temperature depends on the dye and oxidation system. The insoluble vat dye is reduced to a soluble form, absorbed by the fiber, and then oxidized back to its insoluble form inside the fiber. Very high wash fastness and strong durability, especially for workwear, uniforms, denim, and heavily laundered products. Process control is more complex than conventional direct or reactive dyeing. Monitor reducing agents, oxidation, wastewater color, and shade matching. Typically excellent wash fastness; light fastness is often good, but performance varies with the specific vat dye and shade.
Sulfur Dyeing Cotton Denim Workwear Often approximately 60–80°C during dye application, followed by oxidation and washing. Uses reduced sulfur dyes in an alkaline reducing bath. Oxidation converts the dye into its insoluble colored form within the fiber. Cost-effective for black, navy, brown, olive, and other deep shades; suitable for durable cotton articles. Reducing and oxidizing chemicals require controlled handling. Buyers should review odor control, wastewater treatment, formaldehyde risk, and shade-to-shade consistency. Good wash fastness after proper oxidation and washing; rubbing fastness may require additional optimization, particularly for deep shades.
Direct Dyeing Cotton Viscose Paper-Grade Cellulose Commonly 70–100°C, depending on the direct dye and substrate. Dye is applied directly from an aqueous bath, usually with electrolyte assistance. It does not require a separate chemical fixation reaction like reactive dyeing. Simple process route, relatively low chemical complexity, and suitable for economical production of many medium-to-dark shades. Unfixed dye must be controlled to avoid bleeding. Consider after-treatments, wash-off performance, and end-use requirements before selecting this method. Wash fastness is generally lower than reactive or vat dyeing unless after-treated. Light fastness depends on the dye class and shade.
Pigment Padding and Curing Cotton Polyester Blends Nonwovens Drying is often around 100–130°C, with binder curing commonly around 140–180°C, depending on the formulation. Pigments remain on the fiber surface and are fixed with a polymeric binder. Padding, drying, curing, and optional softening are typical stages. Works across many fiber types, uses little or no process water for color application, and is suitable for special effects, prints, and economical solid shades. Hand feel, crocking, binder selection, curing energy, and fabric stiffness must be evaluated. Surface coloration may show more abrasion than fiber-reactive methods. Wash fastness can be good when fully cured; dry and wet rubbing fastness depends heavily on pigment concentration, binder, and curing conditions.
Digital Textile Printing Cotton Polyester Silk Polyamide Post-treatment varies: steaming may be around 100–105°C, while pigment systems generally require thermal curing according to the ink specification. Ink is deposited digitally without conventional rotary screens. Pretreatment, printing, drying, and fiber-specific fixation determine final performance. Excellent for short runs, sampling, complex artwork, personalization, and reduced screen preparation time. Confirm fabric pretreatment, print width, color-management system, minimum order quantity, repeatability, and post-treatment capacity. Fastness ranges from moderate to excellent depending on ink type, substrate, pretreatment, fixation, and washing conditions.
Garment Dyeing Knitted Garments Cotton Viscose Blends Usually follows the dye family used; many aqueous garment-dyeing processes operate approximately between 40–130°C. Finished or semi-finished garments are dyed after cutting and sewing. Mechanical action, liquor ratio, and garment loading affect shade and appearance. Allows flexible color changes, reduced fabric inventory, washed effects, and a distinctive casual appearance. Potential risks include seam abrasion, panel-to-panel variation, shrinkage, pocket and trim compatibility, and dimensional instability. Depends on the selected dye system. Buyers should request garment-level wash, rubbing, perspiration, and dimensional-stability test reports.
Solution Dyeing Polyester Nylon Acrylic Olefin Colorant is added before fiber extrusion; there is no conventional post-spinning aqueous dye bath. Pigment or dye is incorporated into the polymer melt or spinning solution, so color becomes part of the fiber rather than being applied afterward. Very strong resistance to washing, light, and chemicals; can substantially reduce water use in coloration compared with conventional piece dyeing. Color changes require polymer and spinning-process planning. It is less flexible for small quantities and late-stage shade changes. Often excellent wash and light fastness, especially for outdoor, automotive, geotextile, and performance applications.

Note: Temperature ranges and performance descriptions are typical industry ranges rather than fixed specifications. Actual results depend on fiber composition, fabric weight, dye class, machinery, liquor ratio, pH, auxiliaries, fixation, washing, and finishing conditions.

Quality Control, Color Matching, and Environmental Compliance

China’s Best Textile Dyeing Process for Global Buyers?

Quality control begins with repeatable preparation, not the dye bath alone. Chinese dye houses should record water hardness, fabric absorbency, liquor ratio, temperature, and machine speed. A 2024 Textile Exchange Materials Market Report recorded 124 million metric tonnes of global fiber production in 2023. This scale makes small process errors expensive. Buyers should approve a lab dip under standard lighting, then compare bulk fabric using spectrophotometer readings and ΔE limits. A visual check still matters.

Color matching needs discipline. A lab dip can look perfect under daylight but fail under store lighting. Testing should include D65, TL84, and incandescent conditions. ISO 105 methods can assess washing, rubbing, perspiration, and light fastness. Factories should retain greige fabric, dyestuff lots, and signed shade standards. Mistakes happen. Some suppliers rely too heavily on one color measurement.

Environmental compliance requires evidence, not attractive claims. UNEP’s Sustainability and Circularity in the Textile Value Chain report estimates textiles create 2–8% of global greenhouse-gas emissions. Dyeing teams should monitor chemical inputs, wastewater pH, COD, color, sludge, and water consumption. The ZDHC Wastewater Guidelines provide useful testing and reporting references. Buyers should request laboratory reports, chemical inventories, discharge permits, and corrective-action records. “Zero discharge” claims need careful verification. A cleaner process may still consume excessive energy or water. Better factories measure both.

How Global Buyers Can Select a Reliable Chinese Dyeing Partner

China Best Textile Dyeing Process for Global Buyers?

Selecting a reliable Chinese dyeing partner requires more than comparing price lists. Ask for production records, laboratory reports, and clear explanations of shade control. A capable mill should provide lab dips, bulk approval samples, and test results for colorfastness, shrinkage, and fabric weight. Request a factory visit or a live video inspection. Look closely at dyeing vessels, water treatment areas, and fabric storage. Clean floors are not enough.

Experience matters during trial orders. Start with a controlled batch before committing to large volumes. Compare the approved sample with fabric taken from the middle and end of production. Check color under daylight, store lighting, and your final retail conditions. Confirm how the partner handles re-dyeing, rejected rolls, and delivery delays. Written records reduce confusion.

Communication reveals operational discipline. A reliable team reports problems early, not after shipment. Ask who controls recipes, approves chemicals, and records machine settings. Traceable batch numbers should connect fabric rolls with dye lots and inspection results. Environmental documentation also deserves careful review, including wastewater handling and chemical management. Documents can look impressive, yet daily practice may differ. That is why independent testing remains valuable.

No partner is perfect. A successful first order may still hide weaknesses in capacity planning. Leave room for corrective action, honest questions, and periodic review. The best dyeing relationship grows through evidence, not promises.

Scroll to Top